How to Choose a Floating Ball Valve for Global Sourcing

Time:2026-09-06 Author:Aria
0%

Choosing a floating ball valve for global sourcing requires more than comparing prices and catalog photographs. The right selection must match pressure, temperature, media, pipe size, and operating frequency. A valve that performs well on clean water may fail with abrasive slurry or corrosive chemicals. Small details matter. Seat material, body alloy, bore design, and stem construction affect service life.

In practical sourcing work, buyers should request complete technical data before contacting manufacturers. Confirm pressure ratings, end connections, fire-safe design, fugitive-emission requirements, and applicable test procedures. Supplier experience also deserves close review. Examine quality certificates, inspection records, material traceability, and sample test reports. An experienced manufacturer should explain limitations clearly, not simply promise universal compatibility. The term Ball Valve Floating Ball may appear in search results, but search language cannot replace engineering verification.

Global projects add further challenges. Regional standards, documentation practices, shipping conditions, and after-sales support can differ considerably. A reliable supplier should provide consistent drawings, inspection plans, packaging details, and replacement-part information. Factory audits and third-party inspections can reduce avoidable risks. Still, no sourcing plan is flawless. Some judgments remain uncertain until valves face real operating conditions. That is why pilot orders, pressure testing, and field feedback deserve attention. A lower purchase price may look attractive today, yet inconsistent materials or delayed support can increase total cost. Careful selection connects technical suitability with dependable supply, practical service, and transparent communication across borders.
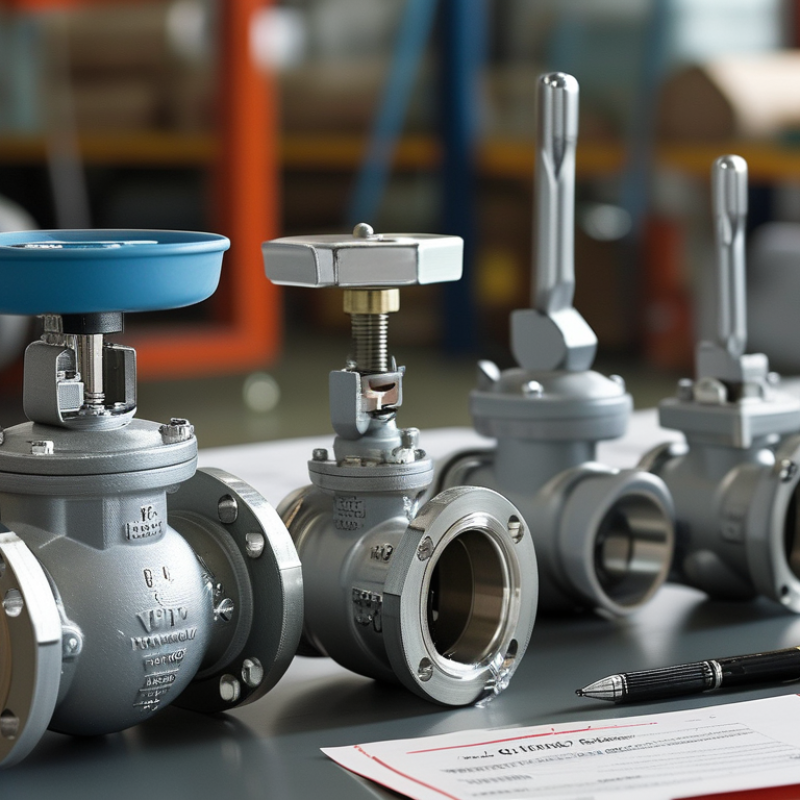
How to Choose a Floating Ball Valve for Global Sourcing

Define Service Requirements: DN, ASME Class 150–2500, Temperature, and Media

How to Choose a Floating Ball Valve for Global Sourcing

Define service conditions before comparing suppliers. Record the line size in DN, operating pressure, design pressure, and temperature range. DN50 may look small, but high-pressure gas service can demand Class 600 or higher. ASME Class 150–2500 is not a simple pressure scale. Its allowable pressure changes with body material and temperature. Verify the pressure-temperature table under ASME B16.34.

Media details matter just as much. Identify gas, liquid, hydrocarbons, chemicals, water, or mixed-phase flow. Note viscosity, solids, chlorides, hydrogen sulfide, oxygen, and abrasive particles. A floating ball valve can provide tight shutoff, but abrasive slurry may damage sealing surfaces quickly. I have seen specifications fail because “oil service” replaced actual composition. That shortcut is risky.

Industry data supports tighter control of emissions. The International Energy Agency’s Global Methane Tracker 2024 estimated about 120 million tonnes of methane emissions from fossil fuel operations in 2023. For such service, request fugitive-emission testing and suitable stem seals. ISO 15848-1 testing can help compare valve performance objectively. Temperature also deserves practical review. Cryogenic service may require extended stems and special seat materials, while high heat can reduce polymer strength. Confirm minimum and maximum temperatures, thermal cycling, fire-safe requirements, and actuator torque. One detail is often missed: pressure drop across the valve. Check it at actual flow, not only at nominal DN.

How to Choose a Floating Ball Valve for Global Sourcing

Reference pressure ratings by ASME class at approximately 38°C (100°F)

Service requirement guidance: Select the valve by defining the nominal size (DN), ASME pressure class, operating temperature, and media. The chart uses approximate carbon-steel reference ratings at 38°C: ASME Class 150, 300, 600, 900, 1500, and 2500 correspond to about 19.6, 51.1, 102.1, 153.1, 255.1, and 425.6 bar respectively. Actual allowable pressure changes with body material, temperature, end connection, sealing system, and applicable standards. Confirm chemical compatibility for the media and verify the required DN, pressure-temperature rating, fire-safe requirements, and leakage class before sourcing.

Match Floating-Ball Design with ISO 17292 and API 6D Requirements

How to Choose a Floating Ball Valve for Global Sourcing

A floating ball valve suits many moderate-pressure applications because line pressure pushes the ball against the downstream seat. This design offers reliable shutoff with fewer moving parts. However, it should not be selected by pressure rating alone. ISO 17292 covers metal ball valves for petroleum, petrochemical, and natural gas services. It addresses design, materials, pressure-temperature ratings, testing, and marking. API 6D focuses on pipeline valves, including functional testing, traceability, and documented performance. The correct standard depends on the service and pipeline role.

A 2024 MarketsandMarkets report estimated the industrial valves market at over USD 78 billion in 2023. It also projected continued growth through 2028, driven by energy, water, and process industries. This scale increases sourcing pressure, but volume cannot replace technical review. Check whether the valve’s floating-ball design matches the specified pressure class, bore, temperature range, and medium. Request material certificates, pressure-test records, fugitive-emission results, and a complete inspection plan. API 6D compliance alone may not confirm every ISO 17292 requirement. That detail is often overlooked.

Tips: Compare the datasheet with the purchase standard line by line. Confirm seat material at minimum and maximum temperatures. Review cavity relief, fire-safe testing, anti-static continuity, and end connections. A certificate pack can look complete yet miss traceability. I would also verify sampling rules independently. It is a small step, but weak documentation can delay customs clearance, installation, or acceptance.

How to Choose a Floating Ball Valve for Global Sourcing - Match Floating-Ball Design with ISO 17292 and API 6D Requirements
Selection Dimension ISO 17292 Considerations API 6D Considerations Global Sourcing Data to Confirm
Primary Application Metal ball valves intended for petroleum, petrochemical and natural-gas applications. Suitable for process isolation when the floating-ball pressure and size limits are acceptable. Pipeline and piping-system valves for petroleum and natural-gas industries. Confirm that the valve configuration and documentation meet the project pipeline specification. State the service medium, line function, installation location, operating cycle, required shut-off direction and applicable purchasing standard.
Floating-Ball Operating Principle The ball is not fixed to a lower trunnion. Line pressure pushes the ball toward the downstream seat, creating the primary sealing force. A floating design may be used where the selected size, pressure class, torque and operating conditions are suitable for pipeline service. Confirm allowable differential pressure, preferred flow direction, seat loading, breakaway torque and maximum operating frequency.
Recommended Size Range Commonly selected for small and medium nominal sizes, subject to the manufacturer’s qualified design and pressure-temperature rating. Floating-ball valves can be used in pipeline applications, but larger sizes and higher pressure classes often require a trunnion-mounted design to control operating torque and seat load. Specify DN or NPS, nominal bore, face-to-face dimension and whether reduced bore or full bore is required. Do not select a size range solely from a catalogue.
Bore Configuration Full-bore and reduced-bore configurations may be available, depending on the valve design and size. Pipeline projects may require full-bore passage for pigging, inspection tools or reduced pressure loss. Record bore diameter, piggability requirement, allowable pressure drop, flow velocity and internal transition geometry.
Pressure Class Typical selections use standardized pressure classes such as Class 150, 300 or 600, where applicable to the design and rating basis. Pressure class, nominal pressure or line-pipe compatibility must match the pipeline design code and the valve’s certified pressure-temperature rating. Specify the rating basis, such as ASME pressure class or PN designation, design pressure, hydrostatic test pressure and maximum operating pressure.
Temperature Range Temperature capability depends on body, seat, stem-seal and bolting materials. Soft seats generally have a narrower temperature range than metal seats. Temperature limits must be compatible with pipeline operating, shutdown, start-up and depressurization conditions. Provide minimum and maximum design temperatures, normal operating temperature, fire exposure requirement and low-temperature impact requirements.
Body Construction Common body options include carbon steel, stainless steel and alloy steel, selected according to pressure, corrosion and temperature conditions. Body materials, pressure-containing parts and manufacturing controls must be suitable for pipeline service and supported by material certification. Confirm material grade, casting or forging route, corrosion allowance, heat treatment, NACE or sour-service requirements and material test certificates.
Ball and Stem Materials Ball and stem materials should resist the process medium, galling and repeated cycling. Stainless or corrosion-resistant alloys may be required. Pipeline service may require documented material compatibility, hardness control and sour-service compliance where hydrogen sulfide is present. Specify base material, overlay or coating, hardness limits, corrosion resistance, stem retention method and traceability to heat numbers.
Seat Material Common soft-seat materials include PTFE-based compounds, reinforced polymers and other qualified thermoplastics. Metal seats may be selected for severe temperature, erosion or fire-service conditions. Seat construction must provide the required shut-off performance over the specified pressure and temperature range. Pipeline isolation duties may require enhanced seat performance. Identify seat material, maximum continuous temperature, chemical compatibility, pressure-assisted sealing behavior and replacement availability.
Sealing Direction Floating-ball sealing normally depends on downstream movement of the ball under differential pressure. Seat design may be unidirectional or bidirectional. Pipeline isolation may require bidirectional shut-off or a specified preferred isolation direction, depending on the system design. Confirm allowable leakage direction, upstream and downstream seat function, cavity relief arrangement and pressure-relief behavior.
Pressure Relief of Body Cavity Thermal expansion of trapped liquid in the body cavity must be considered, especially for liquid service and high-temperature operation. Pipeline valves may require a defined cavity pressure-relief arrangement, such as automatic relief through the seat or an external relief device. Specify self-relieving or non-self-relieving seat behavior, relief-device location, relief set pressure and acceptable cavity-pressure limits.
Fire-Safe Design Fire-safe construction may be required for flammable hydrocarbon service. The valve should use suitable secondary metal-to-metal sealing features and fire-tested components. Pipeline projects commonly require fire-type testing when the valve is installed in flammable-fluid service or where the project specification calls for it. Request a valid fire-test report for the offered design, including size, pressure class, seat material, stem sealing and test configuration.
Antistatic Protection Conductive paths between the ball, stem and body may be required to prevent accumulation of static electricity in flammable service. Antistatic continuity should be verified when required by the pipeline specification or hazardous-area risk assessment. Confirm antistatic construction, continuity test method, maximum resistance value and test records for each production valve.
Stem Retention A blowout-resistant stem arrangement is preferred for pressurized process service and may be required by the purchase specification. Pipeline valves generally require a retained stem design that prevents stem ejection under internal pressure. Check internal or external stem retention, stem shoulder design, gland arrangement and evidence from design drawings or qualification tests.
End Connections Typical options include flanged, threaded, socket-weld and butt-weld ends, selected according to size, pressure class and piping code. Pipeline valves frequently use flanged or butt-weld ends. End dimensions, bore matching and welding details must suit the pipeline system. Specify flange standard and facing, end-to-end dimension, pipe wall thickness, weld-end preparation, corrosion allowance and alignment tolerance.
Actuation and Operating Torque Manual levers or gear operators may be suitable for smaller valves. Floating-ball torque can increase substantially with pressure, seat friction and temperature. Actuators, gearboxes and emergency shutdown systems must be sized for the complete operating envelope, including breakaway and maximum differential pressure torque. Request torque data at minimum, normal and maximum differential pressure, plus safety factor, actuator type, fail position and manual override requirements.
Position Indication Quarter-turn valves should provide clear open and closed position indication corresponding to the ball passage. Pipeline automation may require visual indication, limit switches, position transmitters, valve status feedback and lockable operating devices. Confirm indicator orientation, open/closed travel stops, switch type, enclosure rating, cable entries and hazardous-area certification if applicable.
External Leakage Control Stem seals, body joints and bonnet or end-connection seals must be selected to minimize fugitive emissions and external leakage. Pipeline specifications may include low-emission requirements, packing qualification and enhanced control of stem and body-joint leakage. Specify packing material, emission test requirement, gland adjustment method, body-joint gasket, allowable leakage rate and inspection records.
Testing and Inspection Pressure tests and functional checks should be performed in accordance with the specified standard, purchase order and applicable valve-testing requirements. API 6D projects normally require documented shell and seat testing, operational checks and additional inspection hold points defined by the purchaser. Define test medium, test duration, leakage acceptance, cavity test, low-pressure gas test if required, inspection level and witness or hold points.
Non-Destructive Examination NDE requirements depend on body manufacturing method, material class, pressure rating and purchaser requirements. Pipeline service may require radiographic, ultrasonic, magnetic-particle or liquid-penetrant examination of pressure-containing and weld areas. List examination method, coverage percentage, acceptance criteria, personnel qualification, repair limits and final NDE reports.
Documentation Package Provide dimensional drawings, pressure-temperature ratings, materials, test results, operating instructions and maintenance information. Pipeline procurement commonly requires a complete manufacturing record book with traceability, inspection plans, test certificates and conformity documents. Agree on document index, inspection and test plan, approved drawings, certificates, serial-number traceability, spare-parts list and preservation records.
Corrosive or Sour Service Material selection must account for chlorides, carbon dioxide, hydrogen sulfide, water content, erosion and other contaminants. Pipeline sour-service applications may require compliance with the applicable materials requirements for resistance to sulfide stress cracking and related damage mechanisms. Provide complete fluid composition, partial pressures, water content, pH, contaminants, design life and the required sour-service materials standard.
Maintenance and Lifecycle Cost Floating-ball valves can offer a compact and economical solution, but seat and seal replacement may be needed after high cycling or abrasive service. Pipeline valves should be evaluated for isolation reliability, field maintainability, actuator support, spare-seat availability and planned inspection intervals. Compare purchase price, actuator cost, spare kits, seat and seal life, repair procedure, local service capability and expected delivery time.
Final Sourcing Decision Select the floating-ball design only when pressure, temperature, size, torque, seat loading and sealing requirements are within the qualified design envelope. Use API 6D compliance as part of the pipeline qualification process, not as a substitute for project-specific design, material and testing requirements. Issue a valve data sheet containing size, bore, rating, materials, seats, ends, actuator, testing, documentation and all deviations before quotation approval.
Important sourcing note: ISO 17292 and API 6D requirements can vary by edition, valve configuration and project specification. Always verify the current applicable edition, pressure-temperature tables, purchaser requirements and local regulatory obligations before placing an order.

Verify Materials, Pressure Ratings, and ISO 10497 Fire-Safe Testing

How to Choose a Floating Ball Valve for Global Sourcing

Global sourcing begins with traceable material evidence, not a low unit price. Specify the body, ball, stem, and seat materials separately. Stainless steel may resist corrosion, but chloride service can still cause pitting. Request heat numbers, chemical analysis, and mechanical test records. Confirm the pressure class at the actual operating temperature. A valve marked Class 600 is not automatically suitable for every high-pressure application.

ISO 10497 fire-safe testing checks external leakage, operational function, and pressure containment after fire exposure. The test uses controlled fire conditions, commonly around 750–1,000°C, for a defined period. Ask for the complete test report, not only a certificate number. Seat construction matters because soft materials can degrade quickly. According to the IEA’s World Energy Investment 2024 report, global energy investment was expected to exceed 3 trillion dollars. That scale increases sourcing pressure, but rushed document reviews create costly mistakes. One overlooked temperature limit can invalidate an otherwise impressive datasheet.

Tips: Compare the valve’s pressure-temperature chart with your process conditions. Check whether ISO 10497 testing covers the exact size and design family. Verify ISO 5211 mounting dimensions, end connections, inspection points, and spare-part availability. A perfect document package is uncommon; question unclear revisions, missing signatures, and unexplained material substitutions. During factory inspection, photograph nameplates and measure critical dimensions before shipment.

Compare Suppliers Using ISO 5208 Leakage Grades and API 598 Tests

When choosing a floating ball valve for global sourcing, compare test evidence rather than catalogue claims. ISO 5208 defines leakage rates for valve pressure tests, including closure performance. Lower permitted leakage generally indicates tighter shutoff, but the selected rate must match the service. Do not assume every rate applies equally to resilient and metal-seated designs.

API 598 provides practical inspection and testing requirements for industrial valves. Ask suppliers for shell, seat, and, where applicable, backseat test records. Check the test medium, pressure, duration, valve size, and acceptance criteria. A certificate without these details is weak evidence. In real evaluations, I have seen suppliers pass a visual review while offering unclear test data. That should trigger a technical question, not an immediate rejection.

Tips: Request a completed test report for the exact valve model, size, pressure class, and seat material. Compare the stated ISO 5208 leakage rate with API 598 test results. Confirm whether testing covered both flow directions. Also review sampling controls, calibration dates, and inspector qualifications. Keep written records of every clarification. Small gaps matter. A perfect spreadsheet can still hide inconsistent production. Witness testing may be worthwhile for critical orders, although it adds time and cost. A supplier’s response to difficult questions often reveals more than its sales presentation.

Rank Landed Cost, Certifications, Lead Time, and Global Compliance Risks

When sourcing a floating ball valve, rank landed cost before comparing unit prices. Include the valve, freight, insurance, duties, inspection, warehousing, and possible rework. The World Bank’s 2023 Logistics Performance Index reports an average 44-day journey from export warehouse to import warehouse. That delay can absorb working capital quickly. Ask suppliers for packed dimensions, gross weight, HS classification, country of origin, and realistic production capacity. A low quotation may hide expensive inland transport or oversized packaging.

Certifications deserve a separate risk score. Match pressure class, materials, end connections, and leakage requirements with the destination market. Request current test reports referencing ISO 5208, API 6D, or ASME B16.34, when contractually relevant. Verify heat numbers, pressure-test records, material certificates, and traceability. A certificate alone proves little. Check its scope, issuing body, dates, and product configuration. This step is often skipped.

Lead time should include approval cycles and port congestion. UNCTAD reports that maritime shipping carries over 80% of global merchandise trade by volume, so vessel schedules can affect delivery sharply. Build a schedule with drawing approval, production, testing, export clearance, transit, and customs release. Consider a small safety stock for critical valves. It may look inefficient. Still, a missed shutdown window can cost more than inventory. Compliance screening also needs local review, especially for pressure equipment, environmental rules, labeling, and sanctions controls. The ranking will not be perfect, but documenting each assumption makes revision possible.

FAQS

: Which valve materials should buyers verify?

: Specify the body, ball, stem, and seat materials separately. Request heat numbers, chemical analysis, and mechanical test records. Stainless steel can still pit in chloride service. Do not trust a material label alone.

Does a pressure class guarantee safe operation?

No. Confirm the pressure class at the actual operating temperature. A Class 600 marking does not fit every high-pressure application. Compare the pressure-temperature chart with process conditions. Temperature changes the margin.

What does fire-safe testing examine?

Fire-safe testing examines external leakage, operation, and pressure containment after fire exposure. Controlled temperatures commonly range from 750°C to 1,000°C. Request the complete test report, not only a certificate number. Check the tested size and design family.

How can suppliers be compared through leakage tests?

Use leakage rates and complete test records. The permitted rate must match the service and seat design. Resilient and metal-seated valves may require different expectations. Compare flow directions, pressure, duration, and acceptance criteria. Small gaps matter.

What should a pressure test report include?

It should identify the exact model, size, pressure class, and seat material. Check shell, seat, and applicable backseat tests. Review the test medium, duration, calibration dates, and inspector qualifications. A certificate without details is weak evidence.

How should landed cost be calculated?

Include the valve, freight, insurance, duties, inspection, storage, and possible rework. Ask for packed dimensions and gross weight. Confirm origin, classification, and inland transport costs. A low quotation may hide oversized packaging. That deserves scrutiny.

How should buyers plan realistic delivery times?

Include drawing approval, production, testing, clearance, shipping, and customs release. Port congestion and vessel schedules can change delivery sharply. Consider safety stock for critical valves. It may seem inefficient. A missed shutdown window can cost more.

Which documents and dimensions need checking before shipment?

Verify certificates, pressure records, material traceability, and current revisions. Check mounting dimensions, end connections, inspection points, and spare-part availability. Photograph nameplates during factory inspection. Measure critical dimensions before shipment. Perfect paperwork is uncommon.

Conclusion

Choosing a Ball Valve Floating Ball for global sourcing begins with clearly defining service requirements, including nominal diameter, ASME pressure class from 150 to 2500, operating temperature, and media characteristics. The selected design should align with ISO 17292 and API 6D requirements, while materials, pressure ratings, and corrosion resistance are verified for the intended application. Fire-safe performance should also be confirmed through ISO 10497 testing when required.

Supplier evaluation should go beyond the initial purchase price. Compare valve sealing performance using ISO 5208 leakage grades and review API 598 testing procedures, inspection records, and documentation quality. A practical sourcing decision should rank total landed cost, certifications, production lead time, export documentation, and compliance risks across target markets. By balancing technical suitability, verified quality, delivery reliability, and long-term operating value, buyers can select a floating ball valve solution that supports safe, efficient, and consistent global procurement.
Aria

Aria

Aria is a dedicated marketing professional with a deep passion for innovative strategies and a keen understanding of our company's product offerings. With a wealth of experience in the industry, Aria excels at crafting engaging content that highlights the unique features and benefits of our......