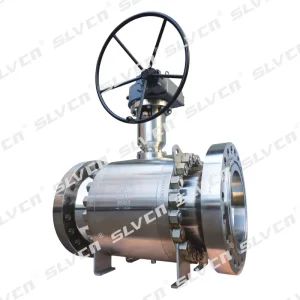
Direct factory supply engineered to API 6D, API 607, and ISO 15848-1 standards for high-pressure, extreme-temperature environments.
Industrial isolation valves represent the fundamental safety barrier across modern energy, chemical, and utility infrastructures. Designed to halt the flow of process media completely under strict operational constraints, these precision flow-control mechanisms prevent catastrophic pressure surges, environmental contamination, and media loss during maintenance or operational emergencies.
The global isolation valve market is undergoing a rapid technical evolution driven by three macro forces: strict environmental regulations regarding fugitive greenhouse gas emissions, an expanding global Liquefied Natural Gas (LNG) supply chain demanding cryogenic reliability down to -196°C, and rising operational temperatures/pressures in next-generation petrochemical processing units.
Chinese valve manufacturing hubs have consolidated raw forged steel sourcing, advanced multi-axis CNC machining, and automated pressure testing laboratories. As a result, premier Chinese manufacturers like SLVCN deliver heavy-duty isolation valves certified to international standards (API 6D, API 607, ISO 15848-1, CE/PED) with accelerated project delivery windows and exceptional cost-to-performance metrics.
Engineered for extreme pressure ratings (Class 150 to Class 2500) and severe temperature services.
Engineered for Class 900–2500 service, ensuring zero-leakage under extreme pressures in critical upstream and offshore pipelines.
Delivering reliable, bubble-tight sealing at ultra-low temperatures down to -196℃ with extended stems for insulation protection.
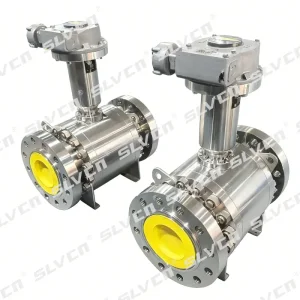
Eliminating body flange leak paths for long-distance buried natural gas transmission and underground trunk pipelines.
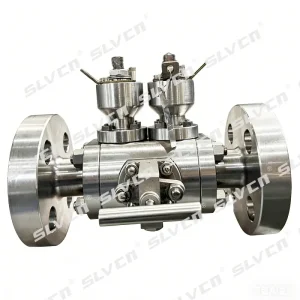
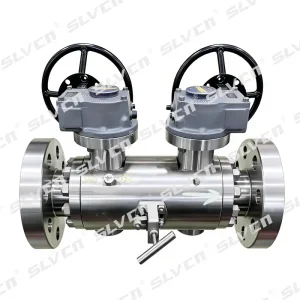
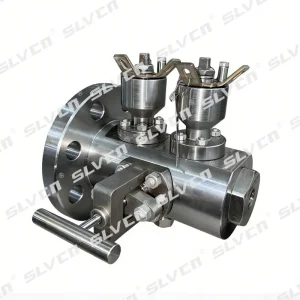
Integrated dual isolation design replacing traditional multi-valve spool pieces to minimize leak points and installation space.
Advanced hard-facing treatments (Stellite, Tungsten Carbide, Chromium Carbide) enabling safe operational cycles up to 550℃.
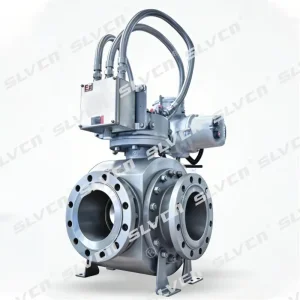
Factory-integrated quarter-turn pneumatic, scotch yoke, and electric actuators for automated emergency shutdown (ESD).
With over 30 years of specialized manufacturing experience in forging high-performance ball and isolation valves, SLVCN provides project-ready solutions tailored to strict global end-user specifications. Our valves are rigorously engineered, non-destructively tested, and certified to perform flawlessly under severe operating conditions.
Trusted by EPC contractors and system integrators across Europe, North America, the Middle East, and Asia-Pacific, our facility combines automated forging lines, 5-axis machining centers, and cryogenic sub-zero testing pits.
Tailored valve material selection, pressure ratings, and sealing technologies tailored for critical infrastructure.
Provides critical pipeline isolation, manifold distribution, and off-shore platform safety shut-off under high-pressure sour gas (H2S) conditions compliant with NACE MR0175.
Delivers exceptional chemical resistance against highly corrosive acids, solvents, and polymers using Hastelloy, Duplex SS, and PTFE/PEEK seating elements.
Specially engineered with extended bonnets to keep stem packing above freezing temperatures, ensuring low operational torque and zero leakage down to -196°C.
Controls high-temperature steam lines, boiler feedwater, and turbine bypass circuits with metal-to-metal seating designed to resist thermal shock and erosion.
Features robust high-pressure isolation valves built with Super Duplex 2507 and Nickel-Aluminum Bronze materials to prevent chloride pitting in seawater RO plants.
Provides ultra-tight gas containment under high pressures (up to 700 bar), utilizing specialized stem seals to prevent microscopic hydrogen atom permeation.
As industrial automation advances toward Industry 4.0 standards, industrial isolation valves are transitioning from simple mechanical cut-off devices into smart, diagnostically aware flow control nodes. SLVCN's R&D department focuses on four core technological vectors:
For abrasive slurries, high-temperature catalytic cracking, and steam isolation above 400°C, traditional soft seals (PTFE/Devlon) quickly degrade. Our engineered valves utilize High-Velocity Oxygen Fuel (HVOF) thermal spraying to apply Micro-Structured Chromium Carbide (Cr3C2-NiCr) and Tungsten Carbide (WC-Co) coatings up to 0.3mm thickness, yielding surface hardness levels exceeding Rockwell C 68.
Environmental compliance under ISO 15848-1 Class AH and EPA Method 21 demands stem leakage rates below 10^-5 mg·m/s. SLVCN isolation valves integrate multi-ring flexible graphite packing set between live-loaded Belleville spring washers. This configuration auto-adjusts for stem thermal expansion and mechanical wear, eliminating the need for periodic manual gland retightening.
When fluid is trapped within the body cavity of a closed double-seated ball valve, ambient thermal exposure can trigger rapid fluid expansion, elevating cavity pressure beyond design limits. Our trunnion valves feature Self-Relieving Seats (Single Piston Effect - SPE) or Double Piston Effect (DPE) seat designs backed by automatic cavity relief valves to guarantee overpressure protection.
Modern plant safety systems (SIS) demand Partial Stroke Testing (PST) to verify valve operation without disrupting plant throughput. SLVCN valve packages support HART and Foundation Fieldbus smart positioners, transmitting real-time operational metrics (torque curves, stem friction trends, seal wear indications) directly to plant DCS platforms.
Rigorous quality control procedures applied across all raw materials, machining processes, and hydrostatic testing routines.
Engineered specifically for extreme-risk, high-pressure, severe temperature, and cryogenic pipelines where operational failure is unacceptable.
Over 30 years supporting international EPC contractors, understanding localized documentation requirements, MTRs, and site acceptance tests.
Every forging and casting batch undergoes 100% positive material identification (PMI), ultrasonic testing (UT), and magnetic particle inspection (MPI).
Fully compliant with API 6D, API 607 (Fire Safe), ISO 15848-1, CE/PED 2014/68/EU, and SIL-3 safety integrity capability certification.
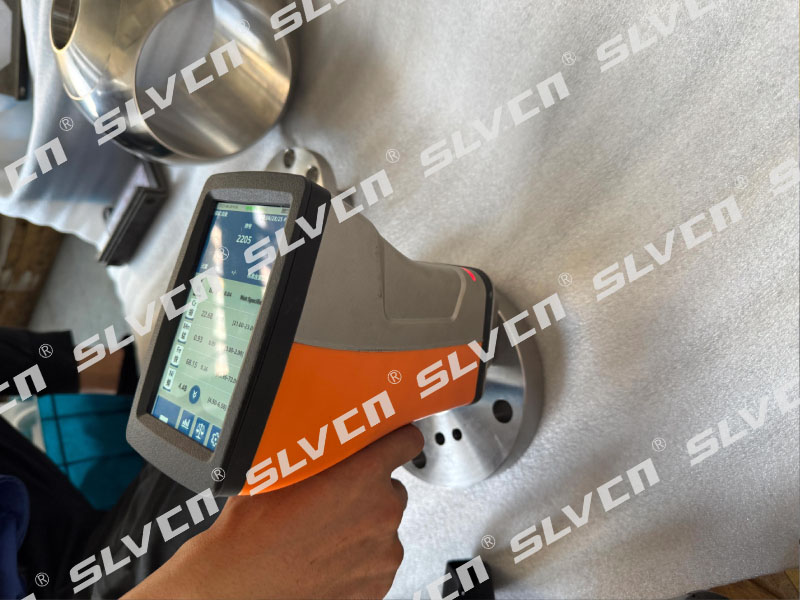
Spectrometric chemistry & mechanical tensile testing for pressure-containing bodies.
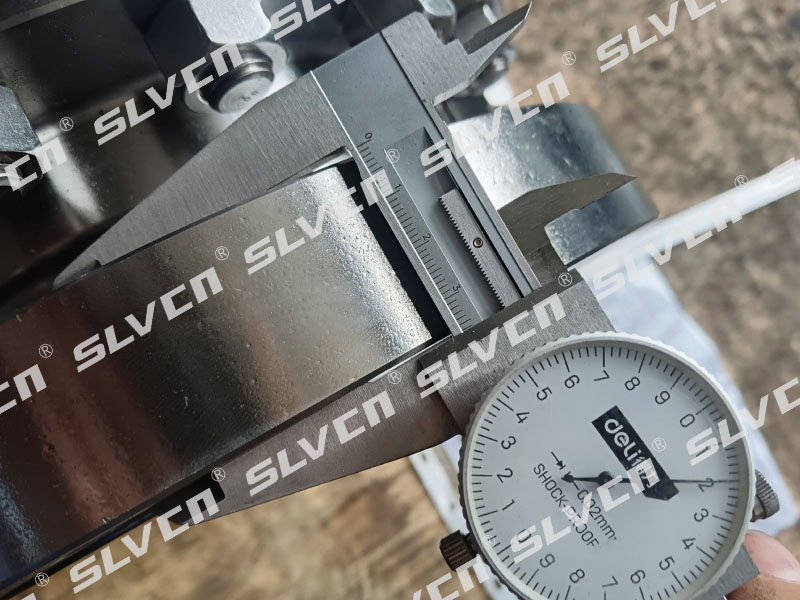
Sub-micron spherical roundness grinding for mirror-finish ball surfaces.
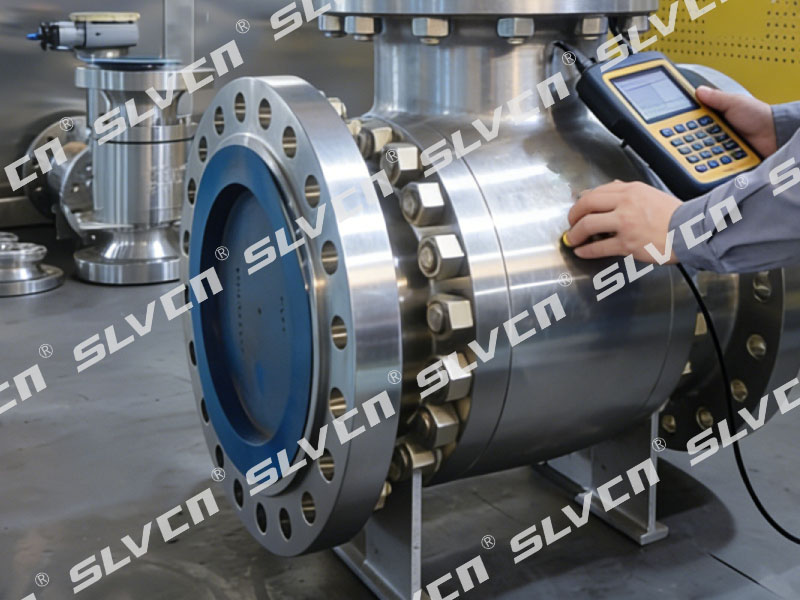
Dust-free cleanroom assembly for oxygen, high-purity, and cryogenic valve trim.
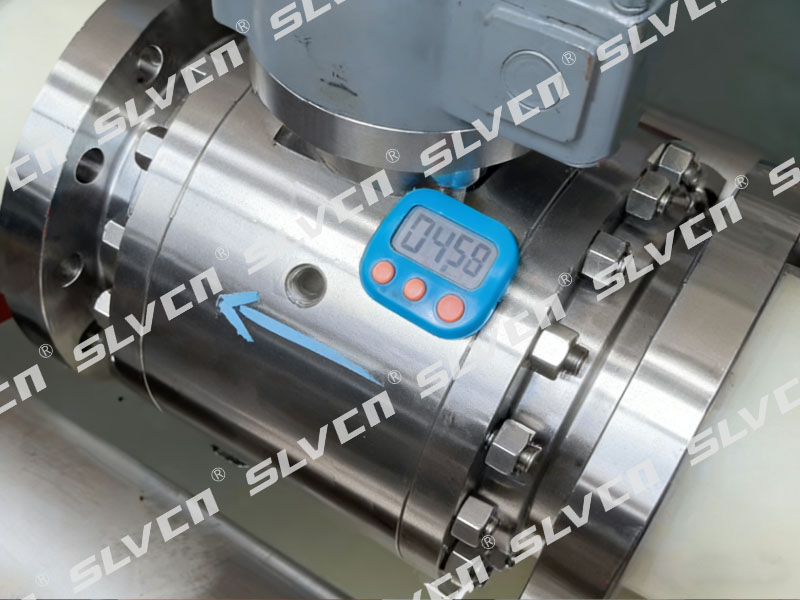
100% shell hydrostatic, seat leakage API 598/API 6D, and high-pressure nitrogen testing.
Proven operational performance in severe industrial installations around the globe.
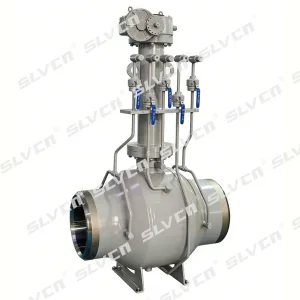
Supplied 24-inch gear-operated fully welded trunnion ball valves with 2-meter extension stems for underground desert transmission lines.
Delivered low-temperature stainless steel DBB valves operating down to -196°C with bubble-tight helium seat leakage certification.
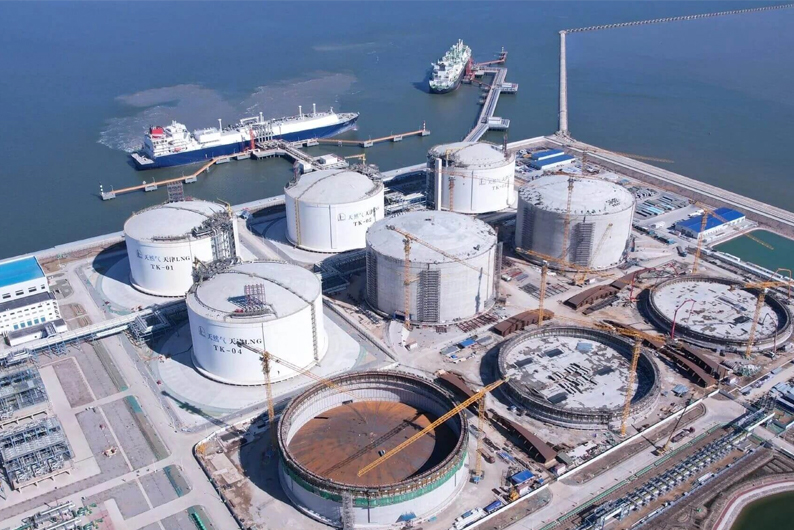
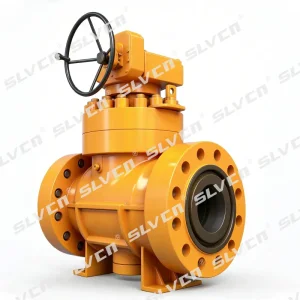
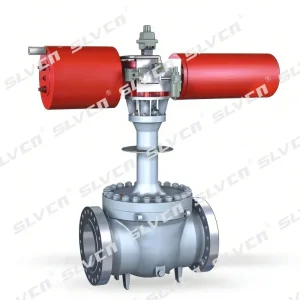
Custom-engineered Top Entry Class 600 ball valves with Stellite hardfacing handling 500°C heavy oil cracking cycles without jamming.
Expert answers regarding isolation valve selection, standards, and Chinese manufacturing advantages.
Stay informed with engineering updates from the SLVCN technical valve team.
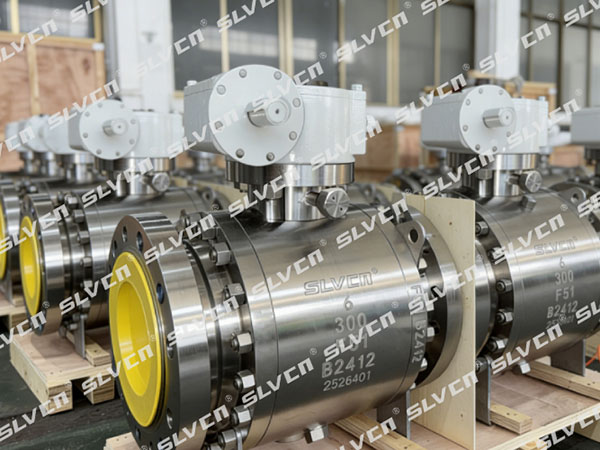
SLVCN is proud to announce the successful shipment of multiple 6" Class 300 RF forged trunnion-mounted ball valves to Southeast Asia.
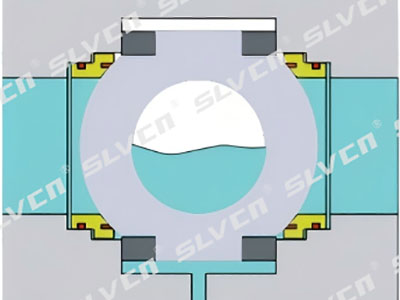
In high-stakes chemical processing and offshore oil platforms, DBB ball valves eliminate traditional spool safety hazards.
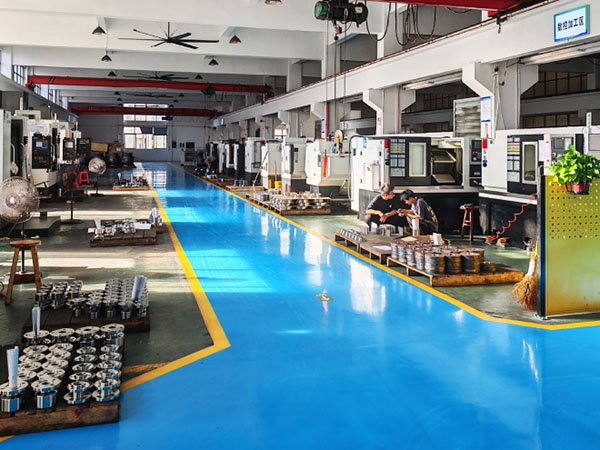
With 30+ years of forging precision, SLVCN provides tailored severe-service valve solutions certified for high safety integrity.
Explore more of our core manufactured product line available for direct factory export.
 Shoulong Valve