China Mechanical Valve Manufacturer & Factory

Global Industrial Whitepaper: Engineering High-Performance Trunnion Ball Valves, Cryogenic Solutions, and Zero-Leakage Flow Control Systems for Critical Infrastructure.

🛡️ Advanced Engineering Core Product Series

Explore our top-tier catalog engineered for extreme pressure, temperature, and zero-leakage safety compliance.

🚀 Executive Summary: The Strategic Evolution of China Mechanical Valve Manufacturing

As a premier China Mechanical Valve Manufacturer & Factory, our operations sit at the intersection of metallurgical science, precision engineering, and global supply chain resilience. Industrial valves are the critical gatekeepers of modern infrastructure—regulating the flow of hydrocarbons, cryogenic fluids, corrosive chemicals, and high-pressure steam. In an era defined by stringent environmental regulations and zero-tolerance safety mandates, global procurement directors demand more than just standard hardware; they require certified engineering excellence, verifiable material traceability, and advanced flow-control architecture.

📈 Mechanical Valve Industry Development Trends: Moving Toward Intelligent Flow Control

The global mechanical valve sector is experiencing a profound technological transformation. Driven by Industry 4.0 paradigms, smart factories, and digital transformation in process plants, several key trends are reshaping manufacturing standards:

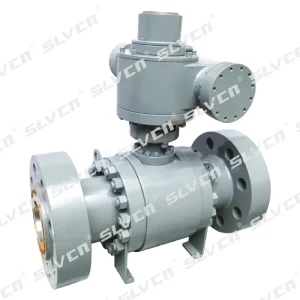
  • Smart Actuation and IoT Integration: Modern industrial pipelines increasingly rely on electric and pneumatic actuated ball valves equipped with diagnostic feedback loops, predicting maintenance intervals before mechanical fatigue occurs.
  • Advanced Metallurgy and Severe Service Coatings: With crude oil souring and chemical processing environments becoming more aggressive, the demand for Tungsten Carbide (WC), Stellite hardfacing, and specialized Inconel/Monel alloys has surged.
  • Stricter Fugitive Emissions Compliance: International standards like ISO 15848 and API 641 dictate that mechanical valves must prevent volatile organic compounds (VOCs) from leaking into the atmosphere, placing immense pressure on stem seal integrity and multi-layer packing designs.

🌍 Global Enterprise Procurement Needs: Mitigating Risk in Critical Infrastructure

Global EPC contractors and Fortune 500 energy conglomerates face unprecedented operational risks. Pipeline leaks in upstream oil & gas or cryogenic LNG terminals can lead to catastrophic financial losses and environmental disasters. Consequently, enterprise procurement criteria have evolved:

  • Total Cost of Ownership (TCO) vs. Initial CapEx: Modern buyers prioritize valves with extended operational lifecycles, reduced maintenance downtime, and proven mean time between failures (MTBF).
  • Comprehensive Certifications: Compliance with API 6D, API 608, CE/PED, ATEX, and SIL (Safety Integrity Level) ratings is non-negotiable for cross-border transactions.
  • Custom Engineering Agility: Standard off-the-shelf valves frequently fail in extreme operating envelopes (-196℃ cryogenic service up to 550℃ high-temperature applications), necessitating agile OEM/ODM manufacturing partnerships in China.

🏭 China Factory 4.0: Supply Chain Resilience & Manufacturing Excellence

China has firmly established itself as the beating heart of global heavy industrial manufacturing. Our production facility leverages state-of-the-art CNC multi-axis machining centers, robotic plasma welding, automated coordinate measuring machines (CMM), and in-house cryogenic/hydrostatic pressure testing laboratories. This vertical integration guarantees unmatched supply chain resilience:

  • Uncompromising Quality Control: Every pressure-retaining forging undergoes Positive Material Identification (PMI) and ultrasonic non-destructive testing (NDT) to eliminate internal casting voids.
  • Optimized Lead Times: By combining streamlined lean manufacturing principles with an extensive inventory of raw forged blocks (A105, F304, F316, F11, Monel), we deliver complex custom valves in a fraction of traditional Western lead times.

🌐 Localized Industrial Application Scenarios & Engineering Mastery

Mechanical valves must perform flawlessly across diverse, demanding industrial ecosystems:

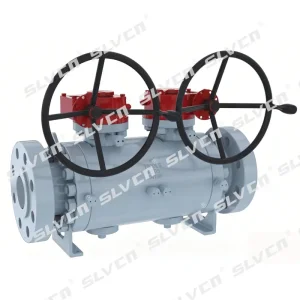
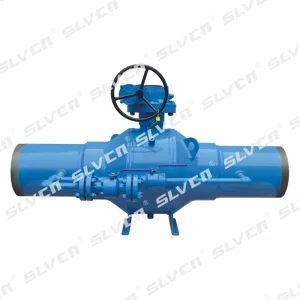
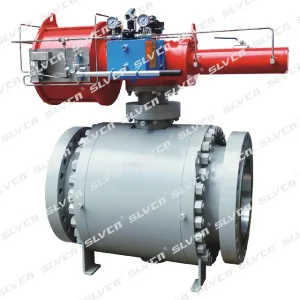
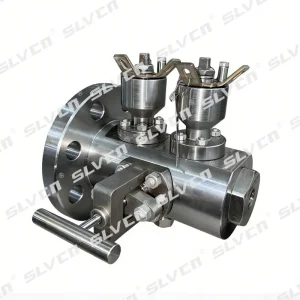
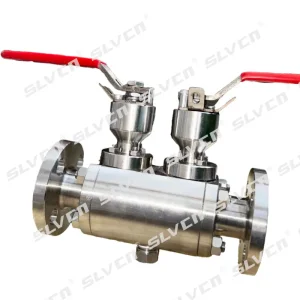
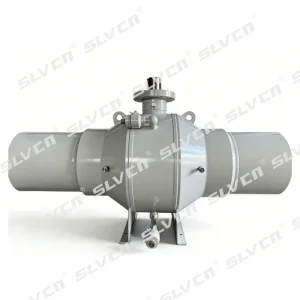
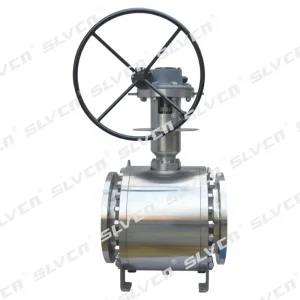
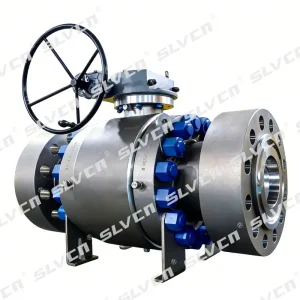
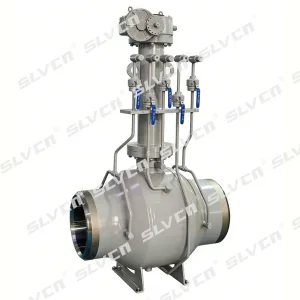
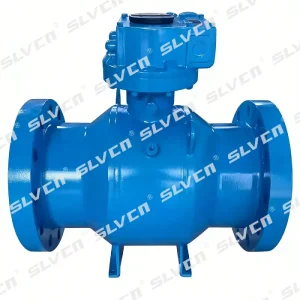
  • Oil & Gas Pipelines (Upstream & Midstream): Utilizing fully welded trunnion-mounted ball valves and Double Block & Bleed (DBB) systems to guarantee secure isolation during pigging operations and high-pressure transmission.
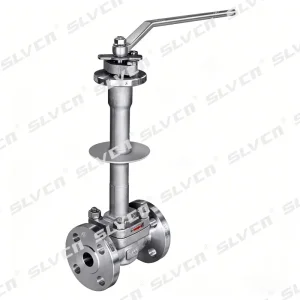
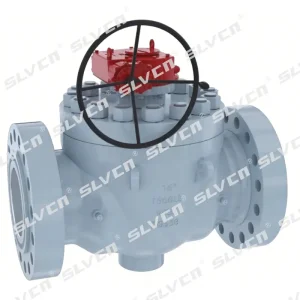
  • LNG & Cryogenic Terminals: Deploying extended-stem top-entry floating and trunnion ball valves designed to insulate packing boxes from ultra-low temperatures (-196℃), preventing stem freezing and leakage.
  • Chemical & Petrochemical Processing: Implementing metal-seated severe service ball valves capable of handling abrasive catalyst slurries and highly corrosive acid streams.

❓ Frequently Asked Questions (FAQ) - Expert Insights for Procurement Professionals

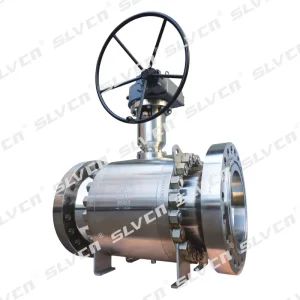
1. What is the primary advantage of a Trunnion-Mounted Ball Valve over a Floating Ball Valve in high-pressure applications?

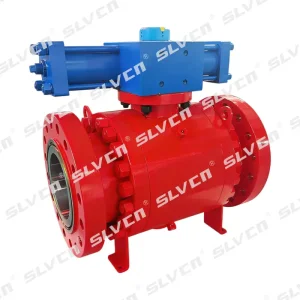
In a trunnion-mounted ball valve, the ball is anchored by mechanical shafts (trunnions) at the top and bottom, meaning line pressure pushes the seat against the fixed ball. This drastically reduces operating torque under high pressures (e.g., Class 900 to Class 2500) and prevents excessive seat wear, ensuring reliable sealing integrity.

2. Why are Double Block & Bleed (DBB) valves critical for pipeline safety?

DBB valves provide two seating surfaces that, in the closed position, isolate the source from the downstream body cavity while offering a bleed (vent) valve between the seats. This allows operators to verify seal integrity and relieve trapped pressure, safeguarding maintenance personnel during critical shutdowns.

3. How do China manufacturing factories ensure international standards compliance?

Top-tier Chinese manufacturers operate under strict ISO 9001 quality management systems and maintain valid API 6D, API 608, and CE/PED stamps. Rigorous shell and seat pressure testing in accordance with API 598 is conducted on 100% of finished valves prior to dispatch.

4. What documentation is provided with industrial valve shipments for major overseas projects?

Complete Material Test Reports (MTRs) per EN 10204 3.1, NACE MR0175/MR0103 compliance certificates for sour service, hydro-test charts, PMI inspection logs, and certificate of origin are standard deliverables for project-grade shipments.

⚡ Specialized High-Pressure & Cryogenic Valvular Solutions

Continuing our comprehensive product lineup tailored for severe service conditions and extreme environments.

🌐 Global Trust Built on Engineering Metrics

Our commitment to precision engineering and global export reliability quantified.

30+

Years of Manufacturing Expertise

100+

Countries Served Worldwide

1,500+

Industrial Enterprise Clients

10,000㎡

Advanced Production Facility