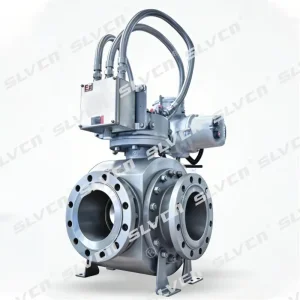
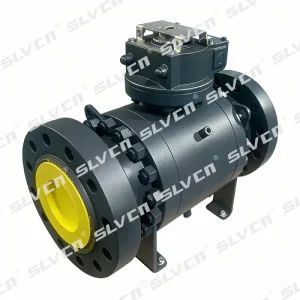
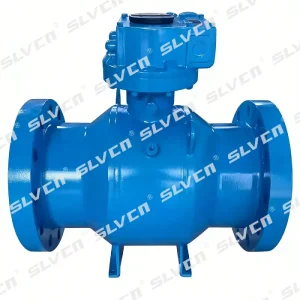
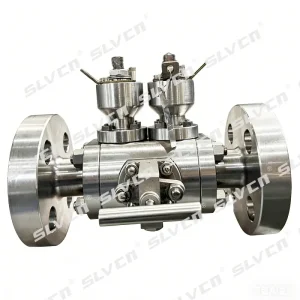
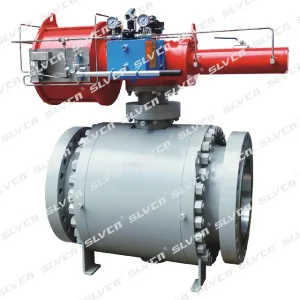
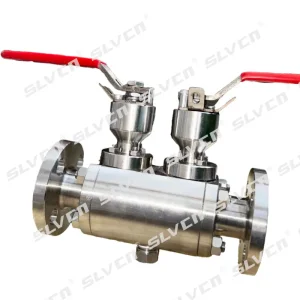
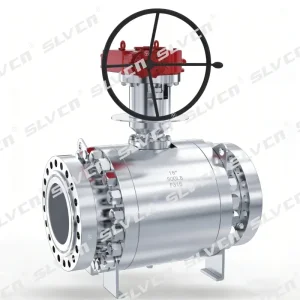
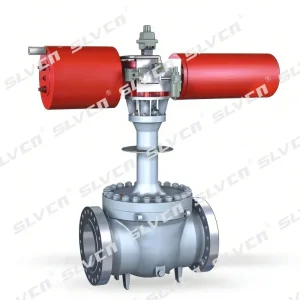
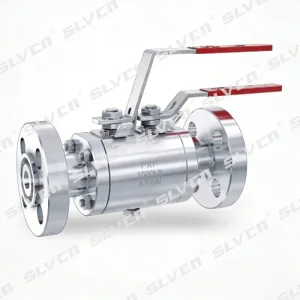
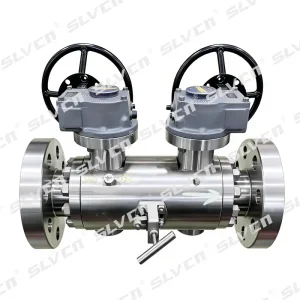
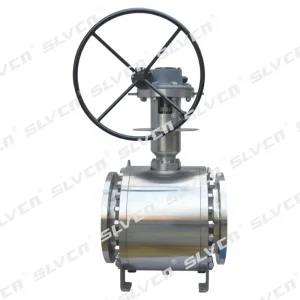
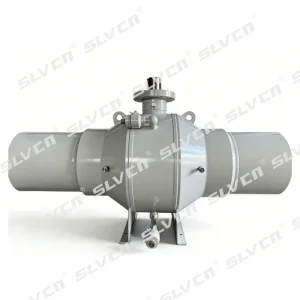
Trunnion Mounted Ball Valve Manufacturers & Supplier in Naples

Engineering High-Integrity Industrial Flow Solutions & Advanced DBB Technology for Global Operations

Advanced Industrial Ecosystem and Trunnion-Mounted Ball Valve Standards in Naples

As a pivotal commercial and maritime hub, Naples presents unique engineering demands across its industrial complexes, fuel distribution terminals, water desalination units, and chemical processing facilities. Modern fluid control systems require high-integrity components capable of withstanding aggressive environments, high mechanical stress, and strict environmental safety thresholds.

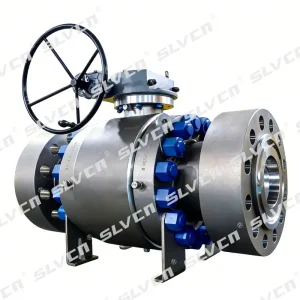
Our engineering division specializes in manufacturing advanced trunnion-mounted ball valves and Double Block & Bleed (DBB) systems. Unlike floating ball valves, trunnion-mounted configurations anchor the ball at the top and bottom, absorbing high line pressures directly through fixed mechanical bearings. This drastically reduces operational torque and prevents excessive seat wear under high-pressure classes ranging from Class 300 to Class 2500.

Why Global Procurement Leaders Partner with Chinese Manufacturing Excellence

Sourcing industrial valves directly from advanced manufacturing bases in China offers global engineering firms and regional project managers in Naples unprecedented strategic advantages. By combining precision CNC machining, automated robotic welding, and stringent quality validation protocols (such as API 6D, ISO 9001, and CE/PED certifications), Chinese industrial valve manufacturers deliver uncompromising reliability at optimal total cost of ownership.

Furthermore, customized manufacturing capabilities allow plant operators to specify exact material grades—including forged carbon steel (ASTM A105N), stainless steel (F316, F304), duplex stainless steel, and Inconel alloys—tailored precisely to corrosive marine conditions or high-temperature steam lines.

Global Valve Industry Trends and Macro Industrial Solutions

The industrial valve sector is undergoing a profound transformation driven by digital automation, stringent fugitive emission regulations (such as ISO 15848), and the transition toward green energy carriers like hydrogen and liquefied natural gas (LNG). Key macro trends shaping the market include:

  • Smart Valve Integration: Incorporation of intelligent electric and pneumatic actuators with real-time feedback loops for predictive maintenance.
  • Zero-Leakage DBB Designs: Increased deployment of Double Block & Bleed configurations to guarantee absolute isolation during critical maintenance routines.
  • Cryogenic and Severe Service Adaptation: Specialized extended bonnet designs and metal-to-metal hard facing to manage ultra-low temperatures (-196℃) and abrasive high-temperature slurries (up to 550℃).

Whether for massive cross-country natural gas transmission networks or local petrochemical processing plants in Southern Europe and Naples, our macro solutions provide turnkey reliability, ensuring continuous plant uptime and complete regulatory compliance.

Engineered Excellence in Numbers

Decades of dedicated manufacturing expertise backing critical infrastructure worldwide.

30+

Years of Experience

100+

Countries Exported

1500+

Clients Served

10000㎡

Factory Area

Send Inquiry Now

Frequently Asked Questions (FAQ) for Trunnion Mounted & DBB Ball Valves

1. What is the primary difference between a floating ball valve and a trunnion-mounted ball valve?
In a floating ball valve, line pressure pushes the ball against the downstream seat to create a seal, which becomes difficult under high pressure or large diameters. In a trunnion-mounted ball valve, the ball is mechanically anchored by upper and lower shafts (trunnions), and spring-loaded seats are pushed against the fixed ball. This ensures lower operating torque and superior sealing integrity under high-pressure conditions.
2. When should a Double Block and Bleed (DBB) ball valve be specified?
DBB valves are essential in critical process streams, custody transfer lines, and hydrocarbon processing where absolute isolation is required. They allow upstream and downstream seats to isolate the cavity while a bleed valve vents trapped media, verifying seat integrity and ensuring worker safety during maintenance.
3. Are your trunnion-mounted ball valves certified for international projects?
Yes. All our valves are manufactured under rigorous quality management systems compliant with ISO 9001, API 6D, CE/PED, and fire-safe standards (API 607/API 6FA), making them fully acceptable for demanding industrial projects across Europe, the Middle East, and the Americas.
4. How do you ensure zero-leakage performance in high-temperature or cryogenic services?
We employ precision CNC machining, specialized tungsten carbide or Stellite hard-facing for metal-seated high-temperature variants, and extended bonnets with high-purity graphite or PTFE packing for cryogenic applications down to -196℃. Every valve undergoes rigorous hydrostatic and pneumatic shell/seat testing prior to shipment.

Comprehensive Valve Portfolio

Explore our full range of certified industrial ball valves engineered for extreme operating pressures and temperatures.